
The main production line of a high-capacity fiberglass insulation manufacturing facility faced significant challenges due to fine airborne dust and elevated ambient temperatures. This situation adversely affected the control cabinet, which contained delicate variable frequency drives (VFDs) and programmable logic controllers (PLCs), leading to recurrent thermal shutdowns.

The initial cooling system of the plant depended on standard intake fans and paper filters. However, within a matter of days, the filters became entirely obstructed by fine glass fibers and dust particles, leading to internal cabinet temperatures exceeding 115°F (46°C). In a bid to alleviate the situation, maintenance technicians often resorted to opening the cabinet doors and directing conventional floor fans at the components. Unfortunately, this temporary solution exacerbated the problem by dispersing highly conductive and abrasive dust onto the live circuit boards, significantly increasing the safety risks and jeopardizing the integrity of the components.

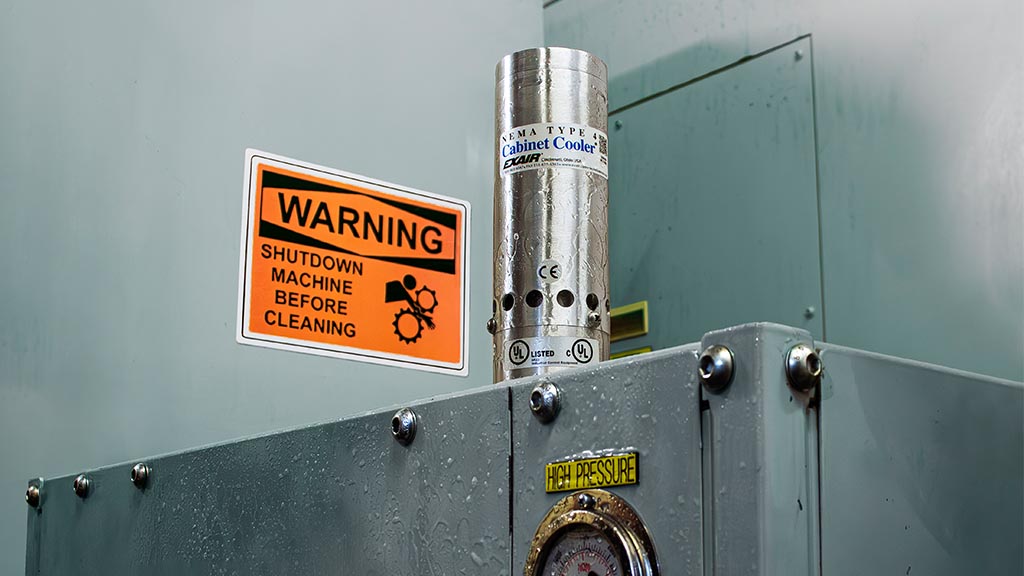
The engineering team, in search of a durable and maintenance-free solution, reached out to an application engineer and subsequently acquired a NEMA 4 NHP Cabinet Cooler System.
The plant staff swiftly installed the compact system within minutes by utilizing a standard electrical knockout located on the enclosure’s top. They effectively sealed the old, leaking fan vents and connected the cooler to the existing factory compressed air line using the provided automatic drain water and dirt filter separator.
The system completely transformed their operational reliability through two distinct phases of automated protection:
- Active Cooling: When the internal cabinet temperature reaches the pre-set thermostat limit, the system’s internal vortex tube transforms the compressed air into a chilled, 20°F (-7°C) airstream without using a single moving part or chemical refrigerant. This cold, clean air was distributed directly onto the hot VFDs, quickly dropping internal temperatures back down to a safe 95°F (35°C).
- Non-Hazardous Purge: Once the target temperature was met, the modified solenoid valve closed but continued to pass a minimal, continuous stream of 1 SCFM of compressed air into the cabinet. This constant airflow maintained a continuous positive pressure inside the cabinet. This positive pressure acted as an invisible shield, physically blocking the fine fiberglass dust from creeping inside through small door seams, wire conduits, or microscopic gaps.
The manufacturer successfully resolved their summer downtime issues by implementing the EXAIR NEMA 4 NHP Cabinet Cooler System. This system ensured that the cabinet remained sealed, free from dust, and maintained an optimal temperature. With no moving parts susceptible to wear, the plant was able to discontinue weekly filter cleaning, enabling maintenance teams to concentrate on ongoing production instead of managing malfunctioning electronics.
If you have questions about the Cabinet Cooler Systems, or anything regarding EXAIR and our products, please do not hesitate to reach out.
Jason Kirby
Application Engineer
Email: [email protected]
Twitter: @EXAIR_jk


